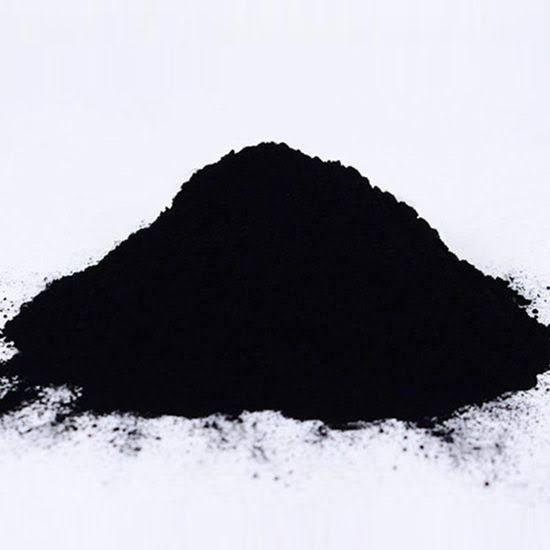
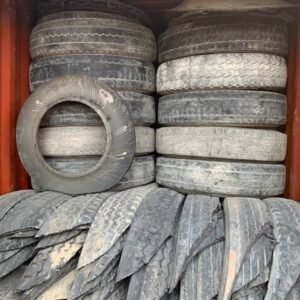
At RB Recycling Group, our Recovered Carbon Black (rCB) is a testament to industrial innovation. Produced through the controlled thermal decomposition of end-of-life tyres, our carbon black is meticulously refined to serve as a sustainable, high-performance alternative to traditional furnace-grade carbon black.
By choosing our rCB, industries can significantly reduce their CO2 footprint while maintaining the structural integrity and pigment quality of their products.
Key Technical Features
-
Reinforcing Properties: Provides excellent tensile strength and abrasion resistance in rubber applications.
-
High Purity: Our advanced post-pyrolysis refining process removes impurities, ensuring consistent particle size and distribution.
-
UV Protection & Pigmentation: Offers superior UV stabilization and deep black coloration for plastics and coatings.
-
Eco-Friendly Profile: Produced with a fraction of the energy and emissions required for virgin carbon black production.
Primary Applications
-
Rubber Compounding: Ideal for non-tire rubber products, including conveyor belts, seals, hoses, and footwear.
-
Plastics & Masterbatches: Acts as a cost-effective pigment and UV stabilizer for PE, PP, and PVC products.
-
Inks & Coatings: Provides consistent tinting strength for industrial paints, coatings, and printing inks.
-
Green Manufacturing: A critical raw material for companies aiming to meet Circular Economy and ESG (Environmental, Social, and Governance) targets.
Why Source from RB Recycling Group?
Our rCB is not just a recycled byproduct; it is a precision-engineered material. We maintain strict batch-to-batch consistency, ensuring that our partners in the rubber and plastic industries receive a reliable supply that integrates seamlessly into their existing manufacturing workflows.
Sustainable. Reliable. Refined. > RB Recycling Group: Closing the loop on industrial carbon.
Reviews
There are no reviews yet.